Tight and reliable sealing leads to process safety and continuous operation of chemical plants
Aggressive chemicals, high temperatures and high pressures are common challenges in the chemical, rubber, and plastic industry applications.Our chemical sector solutions include gaskets, valves, instrumentation, and associated products, which are industry-leading in terms of quality.
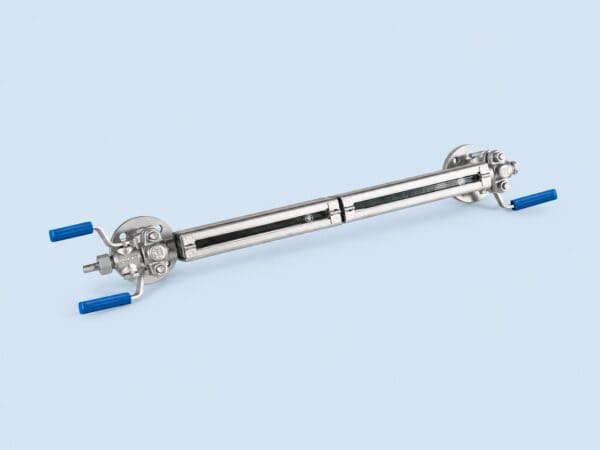
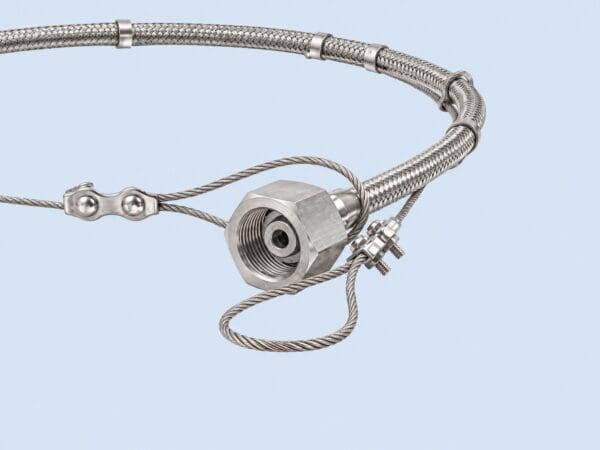
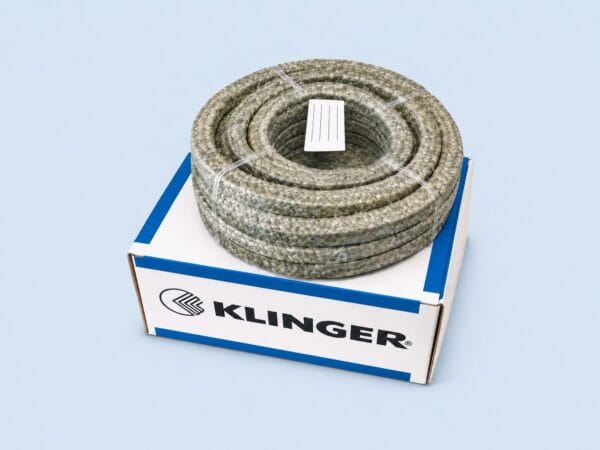
Sealing, fluid control and fluid monitoring technology from KLINGER meets the tall expectations of the chemical and petrochemical industry. A number of plant components that need to be sealed such as pipes and ducts carrying gases and liquids; pumps, agitators and compressors; rotating equipment, fittings and flanges, and more.
As a market leading gasket manufacturer, KLINGER continuously invests in the latest manufacturing technologies to perfect our high-capacity manufacturing processes. This includes advanced IIoT (Industrial Internet of Things) technology and state of the art machinery producing consistent and high-quality products.
Sealing Solutions for the Chemical Industry
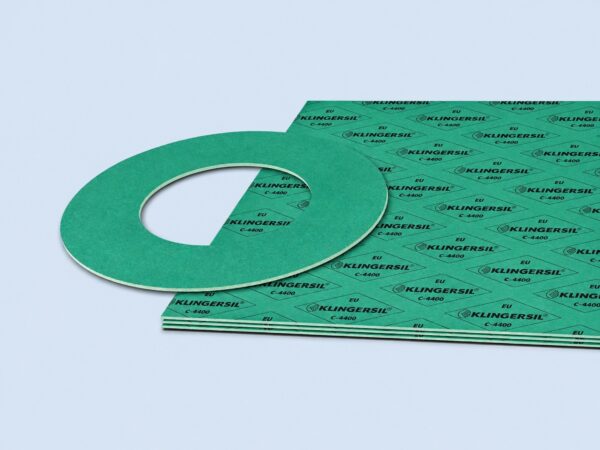
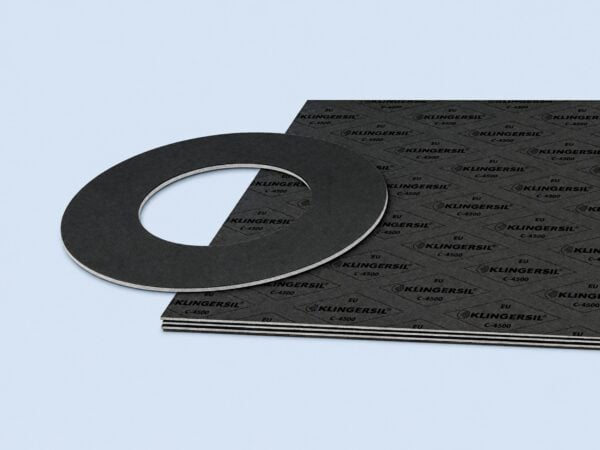
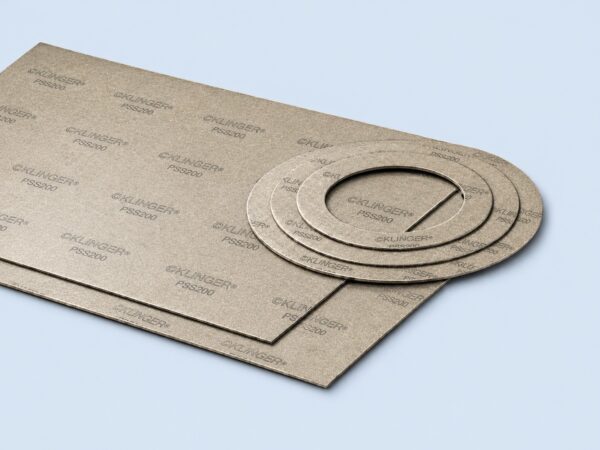
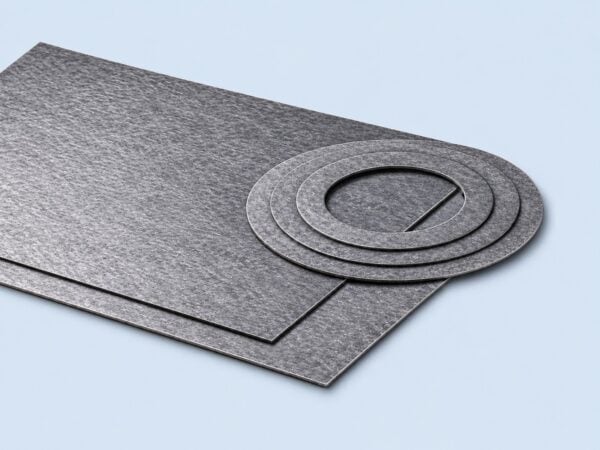
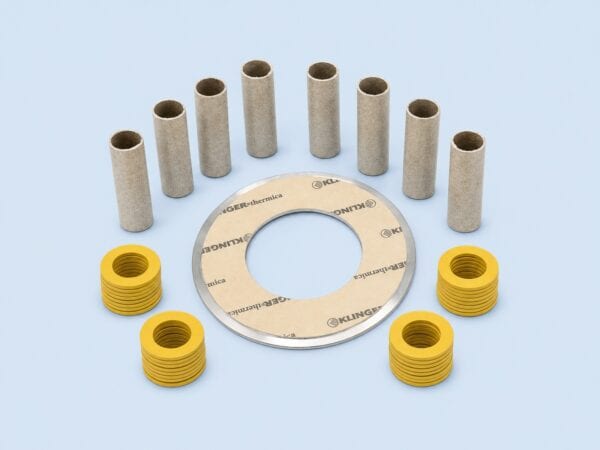
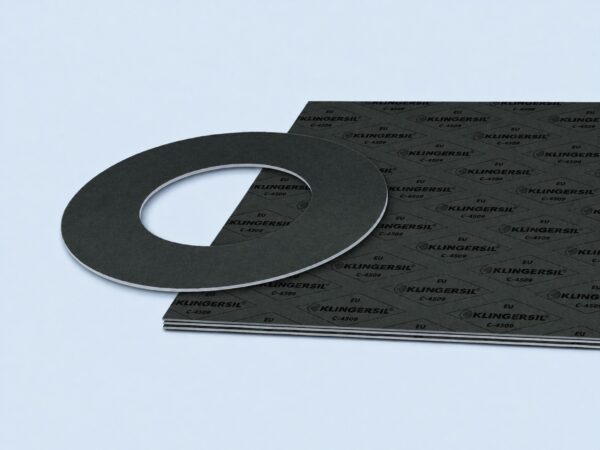
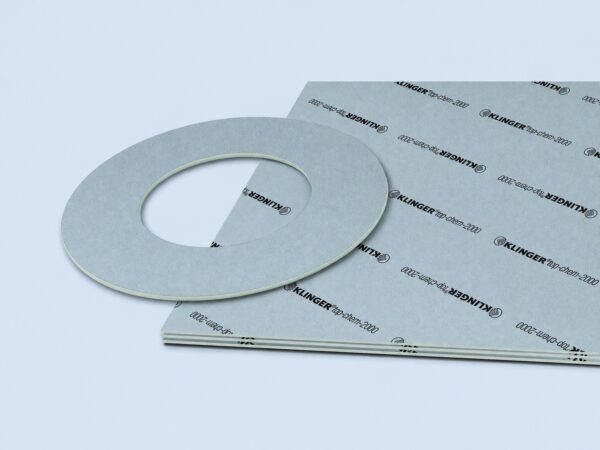
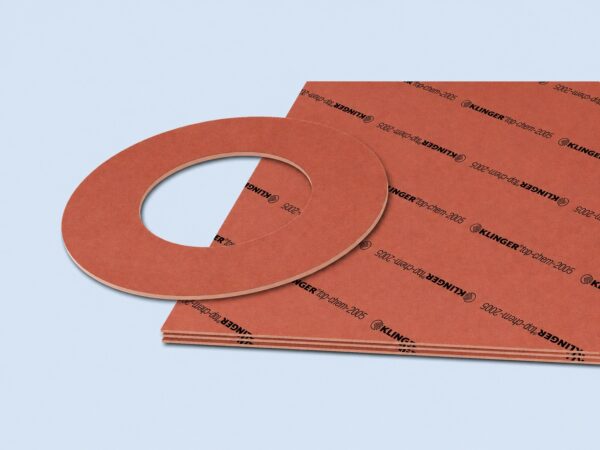
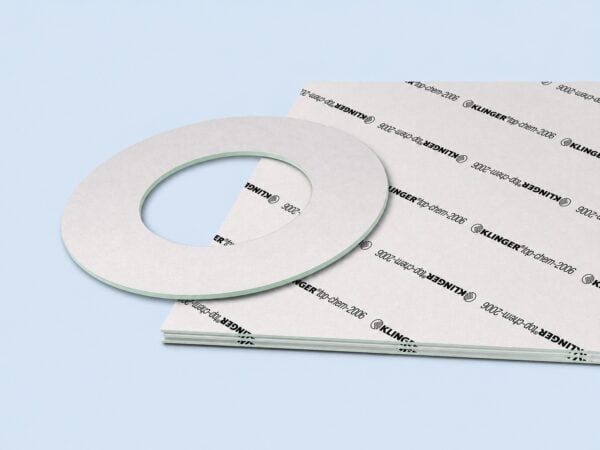
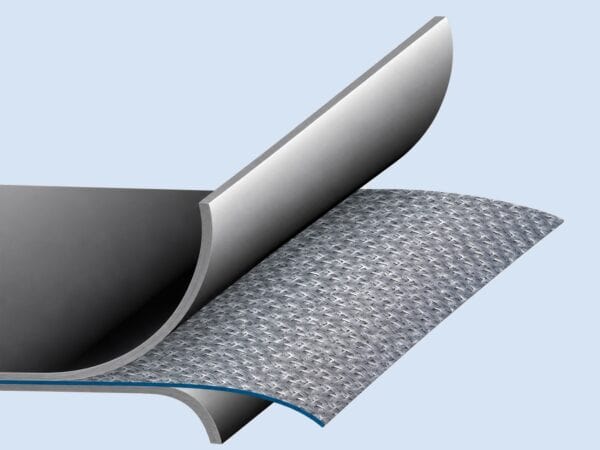
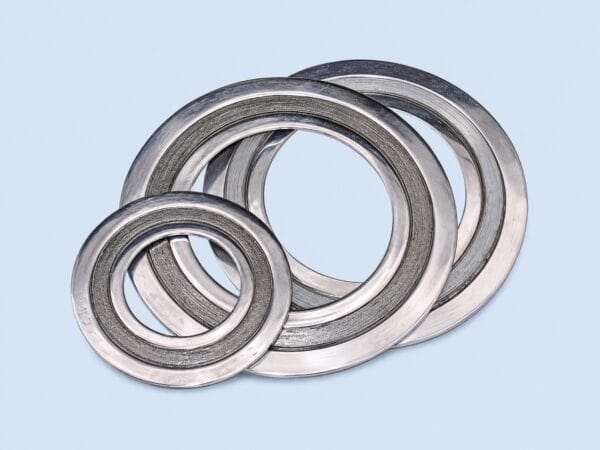
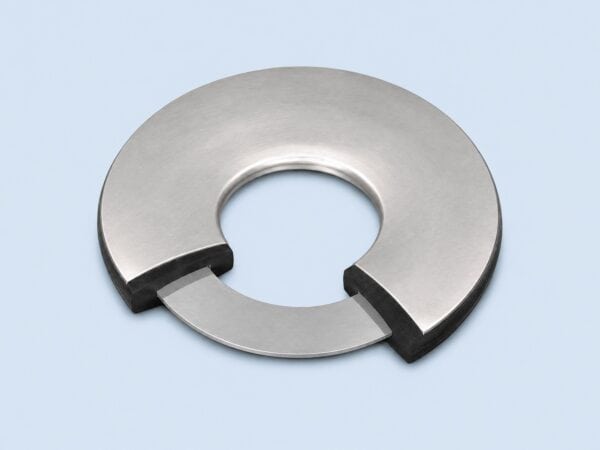
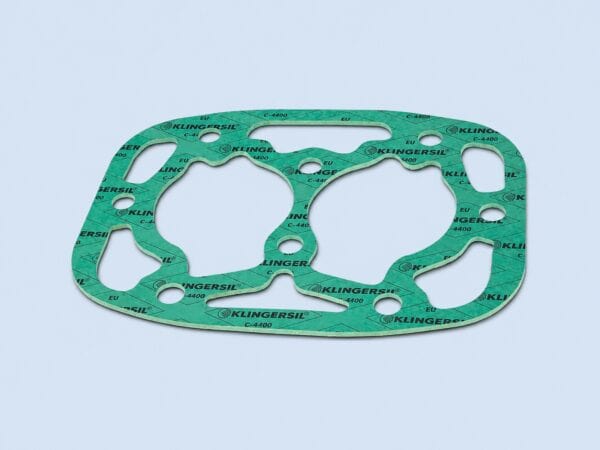
KLINGER sealing products are used worldwide and are well-recognised within the chemical industry. KLINGERSIL, TopChem and SoftChem, specialty KLINGER gaskets, PTFE and PTFE enveloped gaskets are designed for any manufacturing process that requires sealing of aggressive fluids – such as acids and alkalis.
PTFE-enveloped gaskets are particularly useful with aggressive chemicals in the chemical industry, due to their high resistant strength..Only high-quality, non-porous PTFE is used for the envelope, so as to protect the insert against chemical attack.
Valve solutions for the Chemical industry
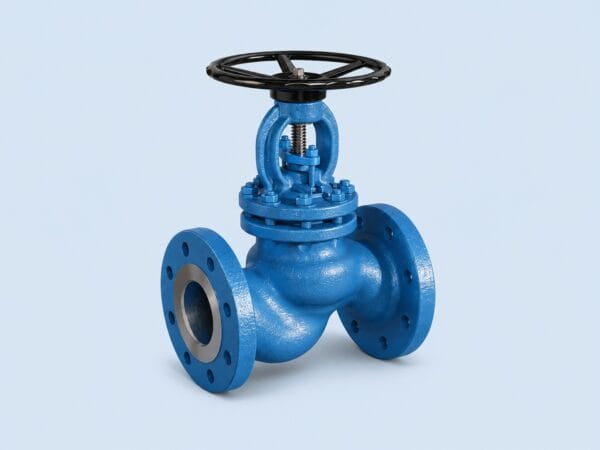
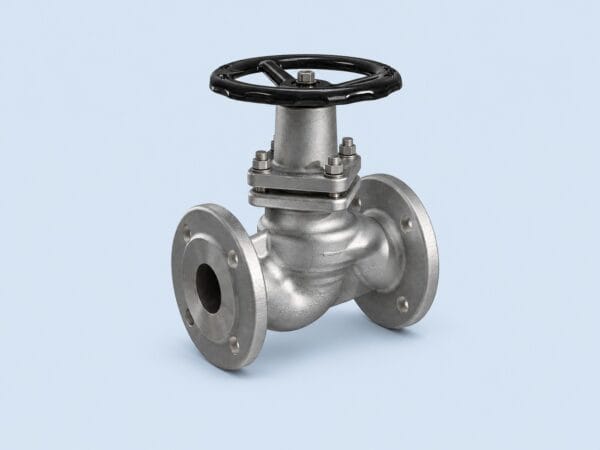
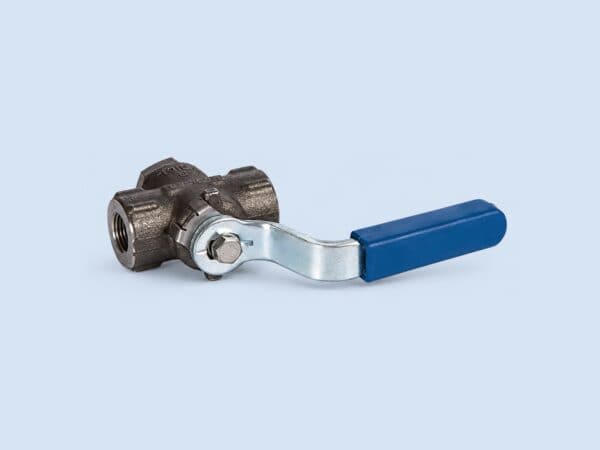
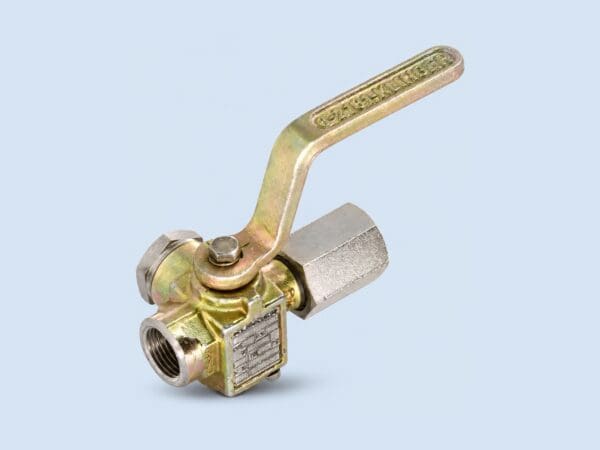
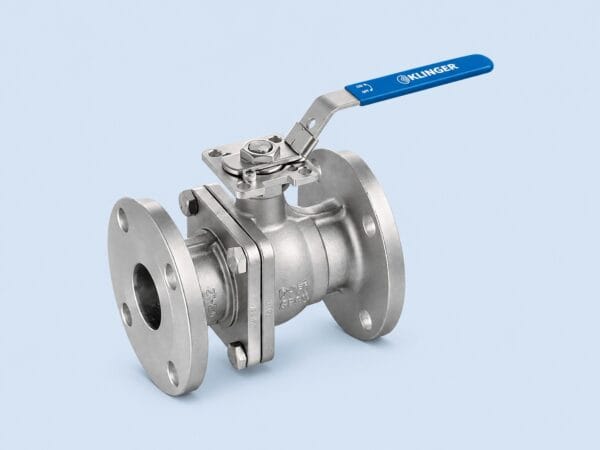
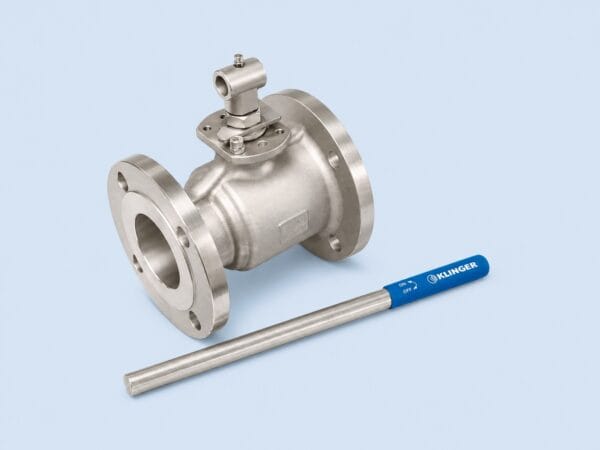
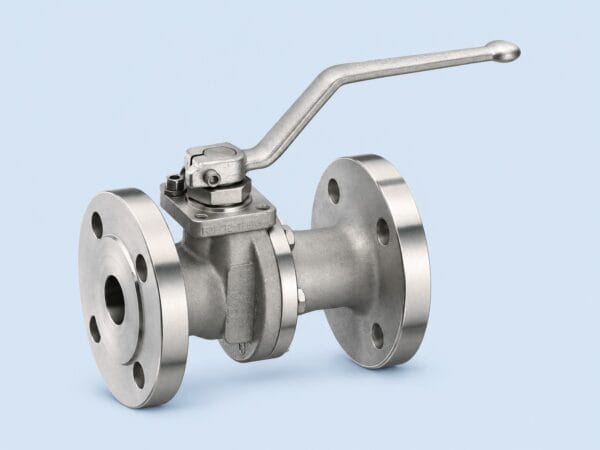
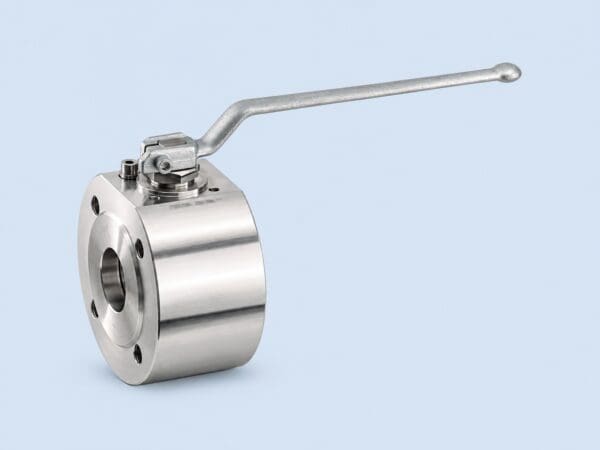
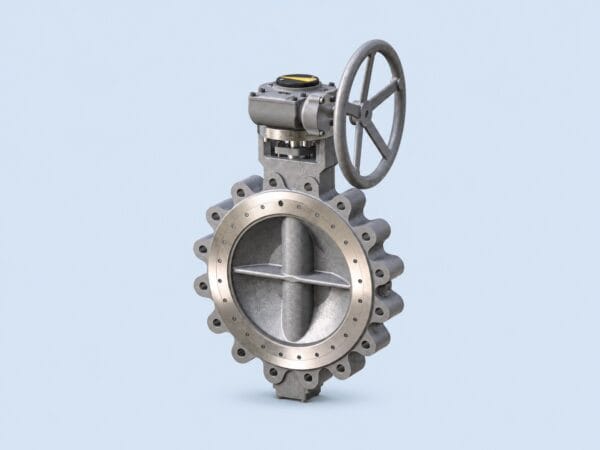
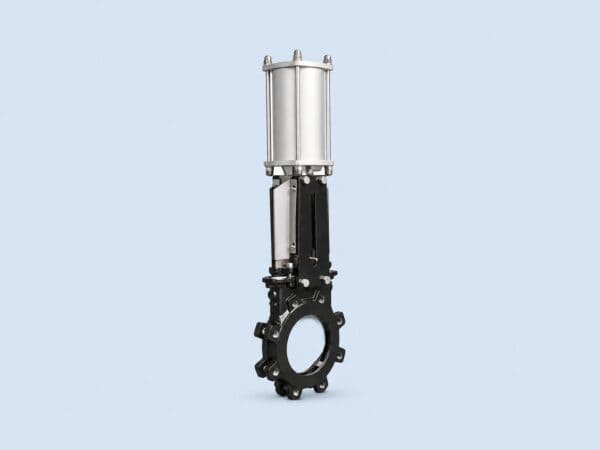
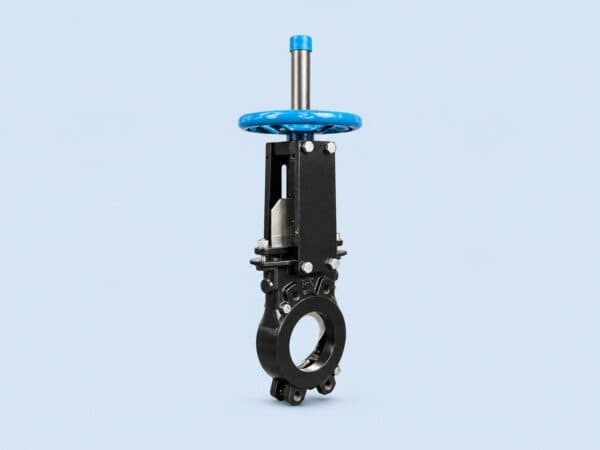
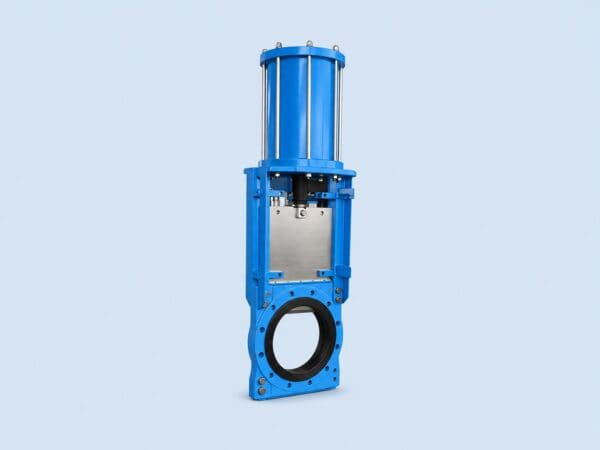
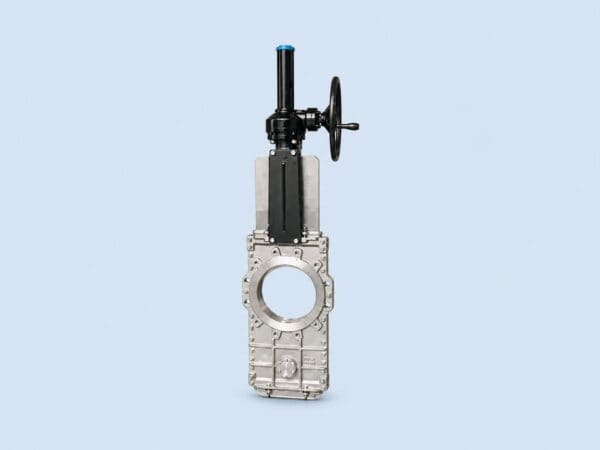
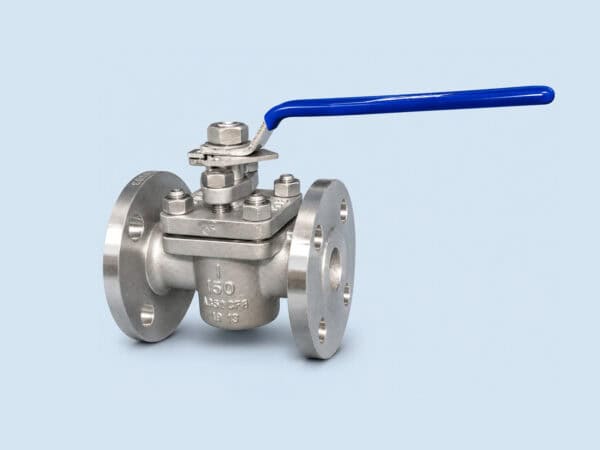
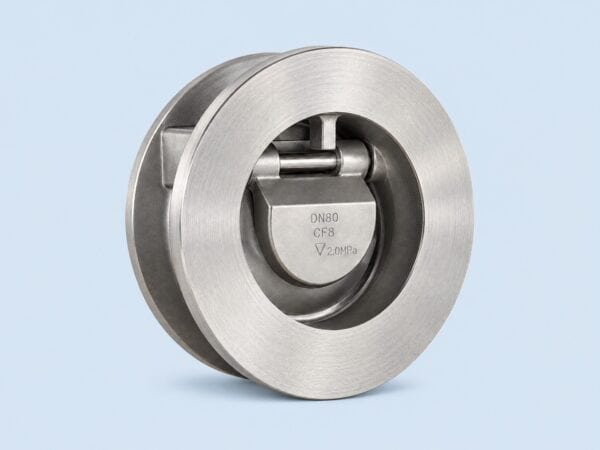
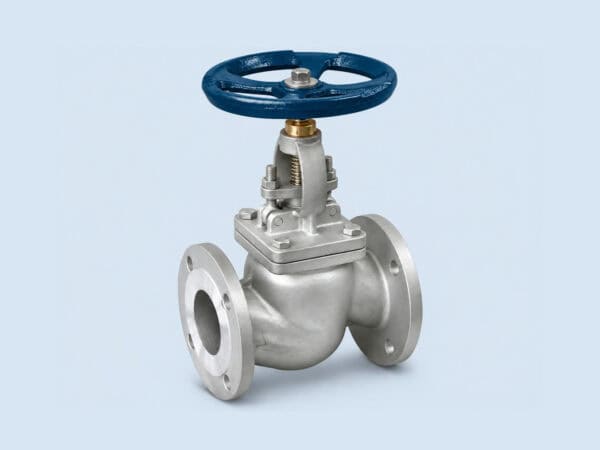
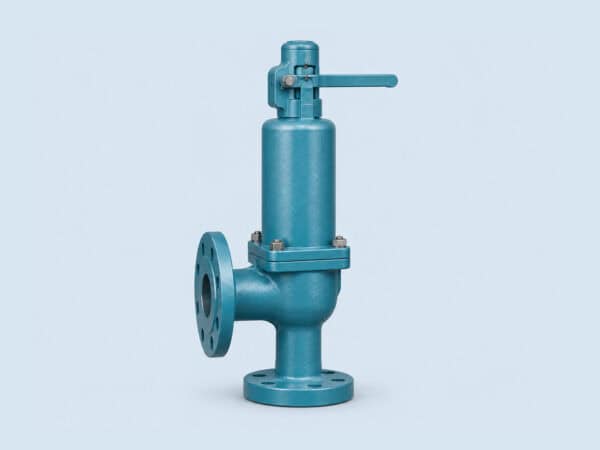
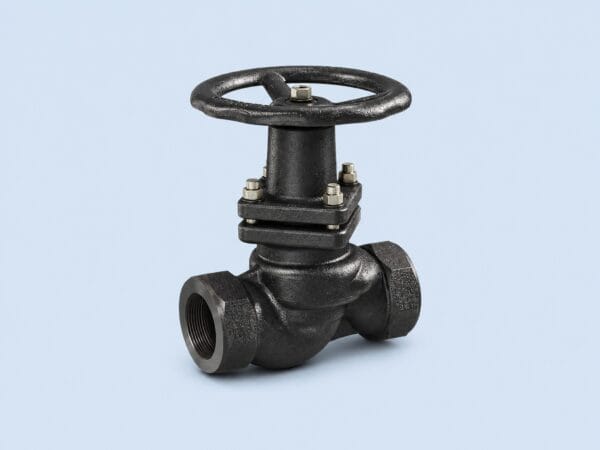
Valves play a huge role in the diverse chemical industry which has thousands of different products. Chemical compounds can be extremely corrosive, abrasive, sticky, volatile or highly toxic substances. The chemical industry needs valves designed for safe, efficient and reliable process operation. From a functional perspective, the industry has a need for control, emergency shutdown, manual/automated on/off, safety and pressure relief valves. Typical valve types used are gate (multiple variations), globe, check, plug, diaphragm, ball, butterfly, as well as plug valves.